Project Overview
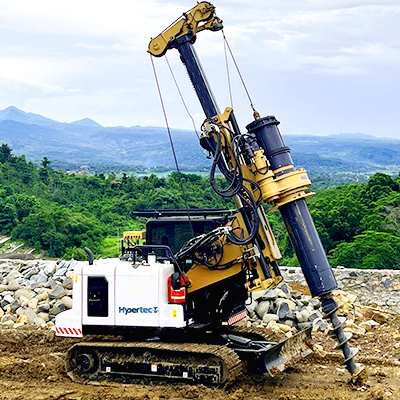
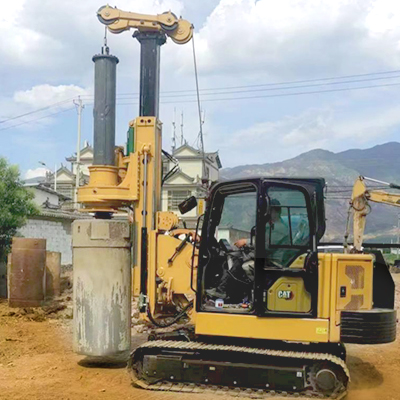
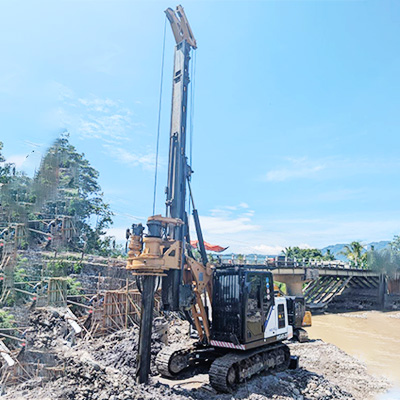
A Class-A general contractor executing a 2-station package of an urban metro line in Southeast Asia approached APIE Foundation Equipment (China) Limited in early 2024. The diaphragm wall scope totaled approximately 18,000 m², with panel depths of 42–48 m and wall thicknesses of 800 mm and 1,000 mm. The original hydromill, fitted with the OEM flat-tooth cutting wheels, was advancing at only 6–8 m²/h in the mid-to-deep sandstone interlayers, and the crew was forced to change the complete wheel set every 900–1,100 m² — a bottleneck that threatened the tunnel boring machine (TBM) handover date. The client sourced a replacement package of cutting wheels for trench cutter from APIE to retrofit the existing hydromill module without buying a new machine.
Challenge
The geotechnical report identified three critical layers: soft to medium clay (0–15 m), dense silty sand with gravel (15–28 m), and moderately weathered sandstone with UCS values of 60–90 MPa and localized basalt dikes reaching 110 MPa (28–48 m). The OEM flat-tooth wheel configuration suffered three compounding problems: rapid carbide tooth loss in the gravel-sand transition, gearbox shock loads when striking basalt inclusions, and verticality deviation exceeding 5‰ once the wheel entered rock — well above the 3‰ contract tolerance. The contractor needed a cutting wheel package that could transition across soft soil and hard rock without a mid-panel wheel change, while keeping verticality within 3‰.
Our Solution
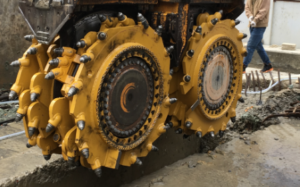
APIE proposed a hybrid wheel package built around our proven hard-rock cutting wheel platform, matched to the client’s existing hydromill gearbox (torque class 150–180 kNm, output speed 0–20 rpm). The delivered configuration included:
- Main cutting wheels with spherical hob (roller-cone) inserts for the rock section — a single hob requires ≥5 t downforce; a 1,000 mm-thick wheel carries 54 hobs with roughly one third (18 hobs) engaged in rock breaking at any time, giving a total rock-breaking pressure of ~90 t per wheel set, within the gearbox’s 45 t per-side radial load rating.
- Pick-drum cutting wheels with tungsten carbide bullet teeth for the upper clay and sand sections, sized 640–1,200 mm to match panel thickness.apiepiling.com
- Reinforced side-cutting wheels (3 per side) and flapper-tooth roller structures engineered to outperform the OEM design in force distribution and to reduce guide-ring wear.
- Matched casing cutter wheel inserts for the guide-wall and joint-cleaning passes.
All wheels shipped with a tapered hexagonal output coupling for 30-minute wheel changeover on site, plus 15% spare hob and tooth inventory for the project duration.
Results & Client Feedback
Over the 14-week retrofit program:
- Average advance rate in rock rose from 6–8 m²/h to 11–14 m²/h — a 40–50% productivity gain directly attributable to the spherical hob cutting wheel configuration.
- Wheel service life extended from ~1,000 m² to ≥1,400 m² per set, cutting wheel-change crane lifts and associated downtime by roughly 30%.
- Verticality of the completed trench was held within 1‰, comfortably inside the 3‰ contract limit.
- Fuel consumption of the carrier power pack dropped to approximately 73 L/h — a saving of over 20% versus the original wheel set.
- The client has since placed two repeat orders covering a second metro line and a drainage caisson project, and has listed APIE as an approved vendor for hydromill wear parts across its regional business units.